Explore our ISO 9001:2015 & CE Certified machinery lineup engineered for deep aquifer access, hard-rock coring, and heavy geotechnical exploration.
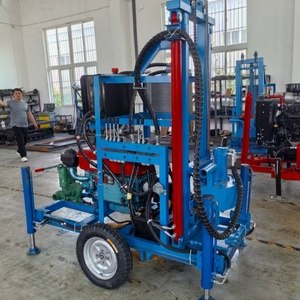
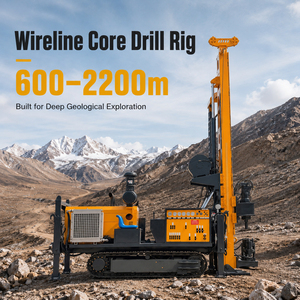
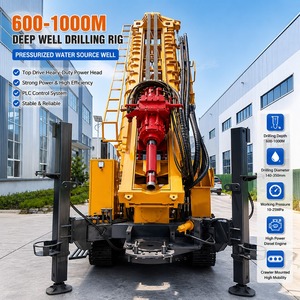
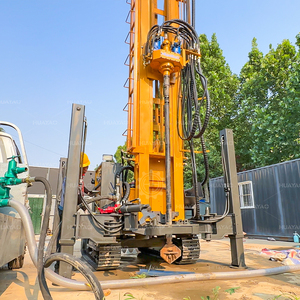
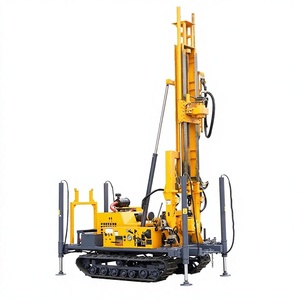
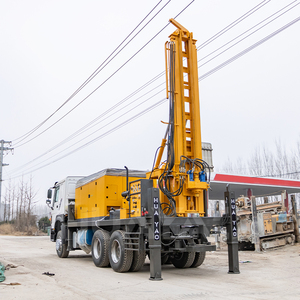
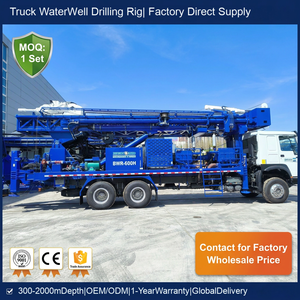
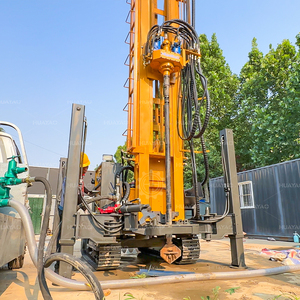
A comprehensive technical report on hydraulic architecture, dynamic load calculations, and geological adaptability for modern geotechnical procurement direct from OEM manufacturers.
Equipped with dual-variable displacement axial piston pumps and load-sensing main valve banks. Reduces engine thermal load by 22% while ensuring constant torque output during deep rock penetration.
Seamlessly switch between high-pressure Down-The-Hole (DTH) air hammer flushing for hard basalt and mud circulation drilling for soft alluvial layers, eliminating the need for secondary machinery.
Fully compliant with EN 16228 drilling safety standards. Features emergency anti-entanglement wire switches, FOPS/ROPS certified operators cab protection, and hydraulic anti-drop safety valves on the mast feed system.
When selecting a drilling rig for deep aquifer penetration exceeding 400 meters, static pull-down capacity is secondary to dynamic rotation torque. In fractured granite formations, friction against the drill string demands a minimum torque coefficient of 18 Nm per meter of depth. Rigs such as our 1000m Truck-Mounted unit deliver up to 22,000 Nm, guaranteeing continuous rotation without pipe lockup.
Contractors and municipal procurement managers must evaluate target lithologies to select the optimal feed rate, flushing medium, and chassis configuration. Below is a engineering guideline compiled by our technical R&D division:
| Target Strata / Geology | Recommended Drill Method | Flush Medium | Ideal Torque (Nm) | Recommended Rig Model |
|---|---|---|---|---|
| Alluvial Clay, Sand & Soft Soil | Mud Rotary / Auger | Bentonite Slurry | 3,500 - 5,000 | HUAYAO 200-H / 300m Crawler |
| Sediment Rock & Sandstone | Roller Cone / Tricone Bit | Air Compressor / Low Mud | 5,500 - 8,500 | 400m Dual Purpose Rig |
| Hard Basalt, Granite & Quartz | DTH Hammer Air Drilling | High Pressure Air (2.5MPa) | 9,000 - 15,000 | 500m Truck / 600m Core Rig |
| Complex Fault Zones (>800m) | Heavy Rotary DTH Combination | High Volume Dual Medium | 16,000 - 22,000 | 1000m Truck-Mounted Diesel Rig |
Key technological transformations shaping the deep water well, core mining, and geothermal drilling machinery sector through 2030.
Environmental regulations across North America, Europe, and Australia mandate reduced particulate matter and NOx emissions for heavy machinery. Future rig procurements strictly prioritize dual-fuel and Stage V compliant diesel powerplants integrated with electronic CAN-bus throttling to reduce fuel burn by up to 18% during idle hydraulic cycles.
Modern commercial drilling contractors require cloud-connected IoT telemetry systems. Integrated sensors monitor real-time penetration rate (ROP), hydraulic pressure spikes, feed force, and engine load. Automated pipe-handling systems eliminate manual labor hazard while logging strata changes digitally for instant hydrogeological reporting.
With surface aquifers depleting globally, municipal and agricultural projects demand wells drilled beyond 500 to 1,000 meters. The industry is witnessing a structural shift toward heavy-duty truck-mounted hydraulic rigs capable of carrying multi-stage heavy drill strings without exceeding legal axle transport weights.
Procurement teams increasingly prefer modular chassis configurations. Off-road exploration contracts favor heavy steel crawler tracks with rubber pads for soft ground mobility, whereas regional infrastructure contractors select 6x4 or 8x4 truck platforms for fast highway transit between municipal well sites.
Combining over four decades of mechanical innovation, rigorous quality controls, and customized OEM/ODM engineering for international B2B buyers.
Every rig frame undergoes high-tensile structural stress testing, Ultrasonic Flaw Detection (UT) on critical welds, and 8-hour continuous hydraulic pressure testing prior to dispatch.
We source top-tier global components including Eaton/Danfoss hydraulic motors, Cummins/Deutz diesel engines, and manganese alloy mast structures built for severe ambient temperatures up to 55°C.
Full export documentation, containerized sea-freight packaging, on-site commission training by field engineers, and guaranteed spare parts availability within 48 hours worldwide.
Clear, authoritative answers to critical engineering, compliance, and ordering queries for global importers.
Connect directly with our senior drill rig design engineers. We provide customized technical proposals, lithological matching evaluations, and competitive direct factory pricing within 24 hours.