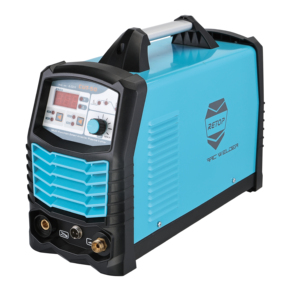
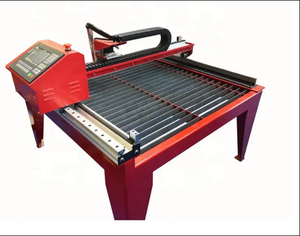
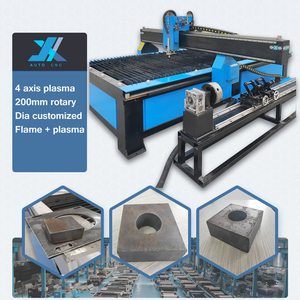
Global B2B Engineering Authority in Precision MIG, TIG, Plasma Cutting Torches, CNC Machining Services & Heavy-Duty Arc Fabrication Systems.
Featured OEM Welding & Plasma Cutting Solutions
Explore our factory-direct industrial catalog. Every torch, CNC cutting machine, and plasma power unit is customizable to exact international engineering standards.
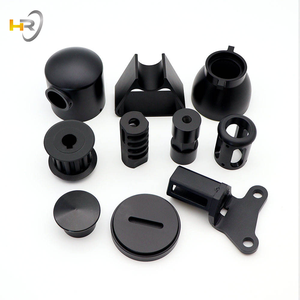
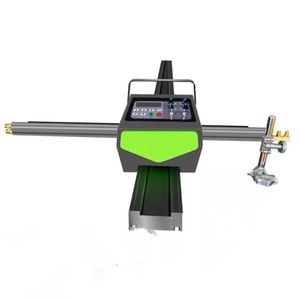
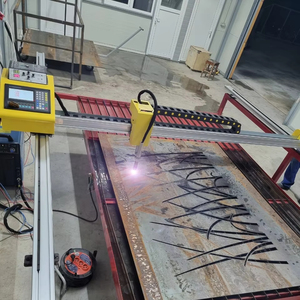
Wholesale Custom Precision CNC Plasma Cutters Steel and Aluminum Parts CNC Machining Services
In modern heavy industrial manufacturing, shipyards, structural steel fabrication, and automotive assembly lines, the performance of the welding torch assembly directly dictates joint integrity, deposition efficiency, and overall operational productivity. As a premier custom OEM welding torch factory and global exporter, our engineering paradigm is built upon four decades of metallurgical mastery, advanced fluid dynamics for shield gas control, and severe-duty thermal dissipation architectures.
Technical Information Gain Insight: The longevity of an OEM MIG, TIG, or Plasma cutting torch depends primarily on the thermal conductivity coefficient of the torch head assembly and the concentricity of its consumable nozzle stack. Sub-par torch heads experience thermal degradation under continuous 100% duty-cycles, leading to gas swirl distortion, arc instability, and high consumable consumption rates.
Whether manufacturing gas-shielded Metal Inert Gas (MIG/MAG) torches, high-frequency Tungsten Inert Gas (TIG/GTAW) guns, or robotic plasma cutting torches, factory customization must address critical environmental stressors. Industrial power grids often exhibit voltage fluctuations exceeding ±15%, while job sites in mining, cement plants, and offshore fabrication expose equipment to high ambient temperatures (up to 55°C) and heavy particulate pollution. OEM torches engineered without severe-duty insulation fail prematurely due to high-voltage arc breakdown or thermal fatigue of internal copper conductors.
Tellurium Copper Alloy Nozzles
Utilizing high-purity C14500 Tellurium Copper for torch nozzles and contact tips ensures 93% IACS electrical conductivity and superior thermal rejection, drastically reducing molten spatter adhesion during high-ampere flux-cored arc welding.
Severe-Duty Insulation
Torch handles and cable bundles utilize high-temperature silicone rubber and dual-layer ballistic nylon sleeves, rated for dielectric breakdown voltages in excess of 10,000V AC, protecting operators and robotic automation cells.
Laminar Gas Flow Diffusers
Precision CNC-machined ceramic and porous brass gas diffusers force shield gas into pure laminar flow profiles. This prevents atmospheric oxygen/nitrogen entrainment, yielding porosity-free radiographic weld seams on stainless steel and aluminum.
OEM / ODM Customization Protocols for Global Procurement
As a certified B2B export manufacturer established in 1980 (operating under the renowned Vulcan brand umbrella), our manufacturing facility caters to private-label equipment brands, global distributors, and EPC contractors. Our OEM customization pipeline accommodates exact electrical, mechanical, and aesthetic specifications:
Connector & Adaptor Interoperability: Custom termination options including Euro-Central, Tweco®, Miller®, Lincoln®, Dinse®, and proprietary fast-disconnect CNC plasma pin configurations.
Coaxial & Water-Cooled Cable Assembly: Production of high-flex coaxial power cables with lightweight outer jackets, micro-switch trigger wiring, and dual-internal water channels for ultra-heavy-duty 600A+ continuous applications.
Ergonomic Torch Body Ergonomics: Custom injection-molded handles engineered with soft-grip rubber inserts, ball-and-socket cable joints, and micro-switch actuation forces under 1.5N to prevent operator Carpal Tunnel fatigue.
Brand & Color Customization: Complete corporate branding services including handle color matching (RAL spectrum), laser-etched logos on torch bodies, customized packaging, and multi-lingual instruction manuals compliant with CE and UKCA directives.
The table below provides procurement managers and welding engineers with a direct comparative breakdown of major industrial torch categories manufactured at our OEM facilities:
Torch Architecture Category
Max Current Capacity
Duty Cycle (EN 60974-7)
Cooling Method
Primary Consumable Alloy
Target Industrial Sector
Air-Cooled Heavy MIG/MAG Torch
180A - 360A CO2 / Mixed
60% @ Max Amperage
Ambient Shield Gas / Air
Tellurium Copper / E-Cu
Automotive, Light Sheet Metal, Fabrication Yards
Water-Cooled Industrial MIG Torch
500A - 650A Continuous
100% Continuous Duty
Closed-Loop Liquid Coolant
Silver-Inserted / CuCrZr Alloy
Shipbuilding, Heavy Structural Steel, Pressure Vessels
High-Frequency TIG (GTAW) Torch
150A - 400A AC/DC
60% to 100% Options
Air & Liquid Cooled Options
Zirconiated / Lanthanated Tungsten
Aerospace, Stainless Pipework, Sanitary Tubing
Handheld Air Plasma Torch (CUT-40/70)
40A - 100A Compressed Air
60% Duty Cycle
Forced Air Flow
Hafnium Electrode / Copper Nozzle
On-Site Maintenance, HVAC Ducting, Demolition
CNC Gantry Automated Plasma Torch
120A - 200A High-Definition
100% Automated Duty
Dual Gas & Water-Jacketed
Hafnium / Silver Electrode Core
Heavy CNC Metal Cutting Workbenches, Water Tables
Future Procurement Trends in Industrial Welding Torches (2025–2030)
As global manufacturing shifts toward Smart Industry 4.0, total quality management, and zero-defect production, the demand expectations placed upon OEM welding torch suppliers are undergoing a radical evolution. Procurement departments must align their supply chain strategies with five key emerging trends over the next decade:
1. Smart Torches with Integrated IoT Sensors
Next-generation OEM torches feature integrated hall-effect sensors, thermal thermocouples, and OLED parameter displays right on the handle. These transmit real-time voltage drops, gas flow rates, and wire-feed friction data directly to central MES platforms.
Utilizing Selective Laser Melting (SLM) 3D copper printing, factory torch bodies can now feature complex internal conformal cooling channels. This improves heat extraction by up to 45% compared to conventionally drilled copper blocks, doubling consumable lifespan.
3. Zero-Dross Dual-Vortex Plasma Nozzles
Cutting torch design is moving toward dual-gas vortex technology. By swirling an auxiliary secondary shield gas around the primary plasma jet, edge dross is virtually eliminated on thick carbon steel plates, drastically reducing secondary grinding labor costs.
Furthermore, sustainability mandates are prompting global buyers to prioritize modular torch design. Modern factories require torch heads where wear components (such as conductor tubes, gas valves, and trigger switches) can be individually replaced in seconds without discarding the entire coaxial cable bundle, reducing industrial e-waste and lowering Total Cost of Ownership (TCO).
Industry Development: Plasma Cutter Integration & Inverter Power Synergies
The rapid miniaturization of IGBT (Insulated Gate Bipolar Transistor) inverter power sources has transformed the plasma cutting and welding machine landscape. Inverter machines operating at frequencies between 20kHz and 100kHz demand matching high-frequency ignition torches that generate zero Electromagnetic Interference (EMI) to nearby CNC electronics.
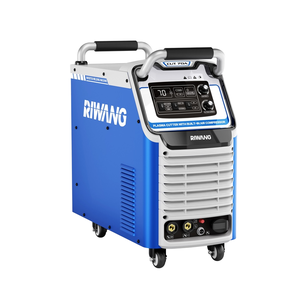
Modern integrated air plasma cutters—such as the CUT-70A and RETOP CUT-40—require custom OEM torches engineered with built-in pneumatic pilot-arc transfer valves. This enables seamless arc starting without relying on high-frequency spark discharge, preventing electronic noise corruption on delicate CNC workbench controllers and automated gantry guidance systems.
Enterprise Authority & Global Manufacturing Footprint
Established in 1980 (founded by Mr. P. M. Vadalia and Late R. A. Patel), Canary Electricals Pvt. Ltd. has grown into an ISO 9001:2015 certified titan in the welding electricals and plasma equipment sector. Operating under our world-renowned Vulcan brand, our manufacturing complex in Morbi, Gujarat, India, supplies buyers across more than 30 countries across Africa, the Middle East, South Asia, and Europe.
Why Global Procurement Officers Partner With Our OEM Factory:
• 100+ Cataloged Machine Models: Complete single-source manufacturing spanning MIG, Spot, Arc, TIG, Thyristorized Rectifiers, Air Compressors, and CNC Plasma Systems.
• Uncompromised Voltage & Environmental Tolerance: Heavy-duty internal coils, varnished transformers, and heat-sink architectures specifically rated to perform continuously in fluctuating electrical environments and high-dust industrial settings.
• Rigorously Certified Quality Assurance: 100% factory dielectric testing, insulation resistance checking, pneumatic leak testing, and thermal load testing before dispatch.
Direct answers to crucial technical and commercial questions raised by international OEM purchasers, importers, and plant engineering leads.
Q1
What primary quality indicators should be verified when sourcing OEM welding torches from overseas factories?
Evaluate three core parameters: 1) Copper alloy purity used in contact tips and torch bodies (demand minimum 93% IACS conductivity C14500 Tellurium Copper); 2) Dielectric insulation rating of handle and outer cable jacket (must withstand >5,000V AC peak); and 3) Duty-cycle verification testing according to EN 60974-7 international standards under ambient temperature conditions (not artificially cooled lab environments).
Q2
How does a water-cooled OEM torch system compare to air-cooled models in continuous high-ampere operations?
Air-cooled torches dissipate excess thermal energy via shield gas and radiant air flow, limiting their continuous 100% duty cycle threshold to roughly 200A-300A. Water-cooled torch assemblies recirculate liquid coolant directly inside the torch head around the tip, enabling continuous 100% duty cycle operation at 500A to 650A+ without thermal handle rise or consumable degradation.
Q3
Can your factory manufacture custom OEM torch assemblies compatible with major European or American machine brands?
Yes. We produce fully interchangeable OEM torch assemblies equipped with standard Euro-Central connectors, Tweco-style terminations, Miller-style pin configurations, Dinse connections, or custom multi-pin signal plugs engineered to match your proprietary CNC or inverter power source specifications.
Q4
What consumable electrode materials are utilized in your high-definition CNC plasma torches?
Our high-definition plasma torch electrodes feature premium Hafnium inserts embedded into high-purity silver-copper composite bodies. Hafnium offers an exceptionally high melting point (2,233°C) and superior electron emission characteristics under compressed air and oxygen plasma gases, delivering crisp kerf angles and extended arc hours.
Q5
What is the typical lead time for customized OEM brand labeling, color packaging, and cable assembly?
Standard OEM prototype samples are typically delivered within 10 to 15 business days. Full production batches with custom injection-molded handle colors, laser-etched private logos, and branded box packaging require a lead time of 25 to 35 days from technical CAD sign-off and deposit confirmation.
Q6
How do integrated air compressor plasma cutters (e.g., CUT-70A) perform compared to external air systems?
Integrated air compressor plasma cutters provide supreme field portability, eliminating the need to haul heavy separate air compressors to job sites. Internal oil-free piston compressors supply instant, tuned pneumatic pressure ideal for sheet metal cut thicknesses up to 20mm-25mm. For heavy multi-shift CNC water table production above 30mm thickness, external high-CFM screw compressors are recommended.
Q7
What measures prevent torch cable breakdown during severe site voltage fluctuations?
Our heavy-duty cable bundles incorporate double-insulated vulcanized rubber inner tubing surrounding ultra-fine braided oxygen-free copper wires. This provides high mechanical flexibility while preventing dielectric breakdown or resistance heating even when input line voltages fluctuate by ±20%.
Q8
What international quality certifications do your manufacturing plants and products hold?
Our parent company, Canary Electricals Pvt. Ltd., is ISO 9001:2015 quality system certified. Products are engineered in compliance with EN 60974-7, CE guidelines, and undergo rigorous factory audits including high-voltage insulation tests, gas leak decay testing, and full thermal endurance runs prior to container loading.
Q9
How does torch gas diffuser design impact weld bead porosity in structural welding?
A poorly machined gas diffuser generates turbulent gas flow, pulling ambient air into the shield stream and creating microscopic weld porosity. Our CNC micro-drilled diffusers enforce smooth laminar gas velocity, guaranteeing 99.9% coverage over the molten weld pool even under cross-draft site conditions.
Q10
What trade terms and shipping options are available for global B2B buyers?
We export under standard INCOTERMS including FOB, CIF, CFR, and EXW. Export cargo is packaged in sea-worthy heavy-duty reinforced corrugated cartons and heat-treated wooden pallets to guarantee zero moisture ingress or damage during transit to ports across Africa, the Middle East, Asia, and America.
Ready to Partner with a Premier Custom OEM Torch Manufacturer?
Contact our engineering export team today for technical CAD consults, private label pricing, and custom OEM sample orders.